
Figuring out what size should a sump pump weep hole be prevents costly motor burnout and basement flooding. Most residential submersible pumps require a precise 3/16-inch diameter bleed hole to relieve trapped air effectively.
Manufacturer specifications indicate this specific dimension balances necessary pressure relief with acceptable water recirculation rates. Drilling arbitrarily larger holes reduces net discharge flow and can void your equipment warranty immediately. Always verify your exact model requirements before modifying any pump casing components.
What Size Should a Sump Pump Weep Hole Be
The standard sump pump weep hole size is 3/16 inch for most residential units. This diameter prevents air locking while maintaining adequate discharge pressure. Some commercial models require a larger 1/4 inch opening for higher flow rates.
Always check your specific manufacturer manual before drilling. Never guess the size based on generic online advice alone.
Why Getting the Size Wrong Risks Pump Failure and Voided Warranties
Incorrect weep hole sizing directly threatens your pump's operational lifespan and warranty status. A hole drilled too small fails to release trapped air pockets inside the discharge pipe. This causes air locking where the impeller spins uselessly against a vapor barrier without moving water.
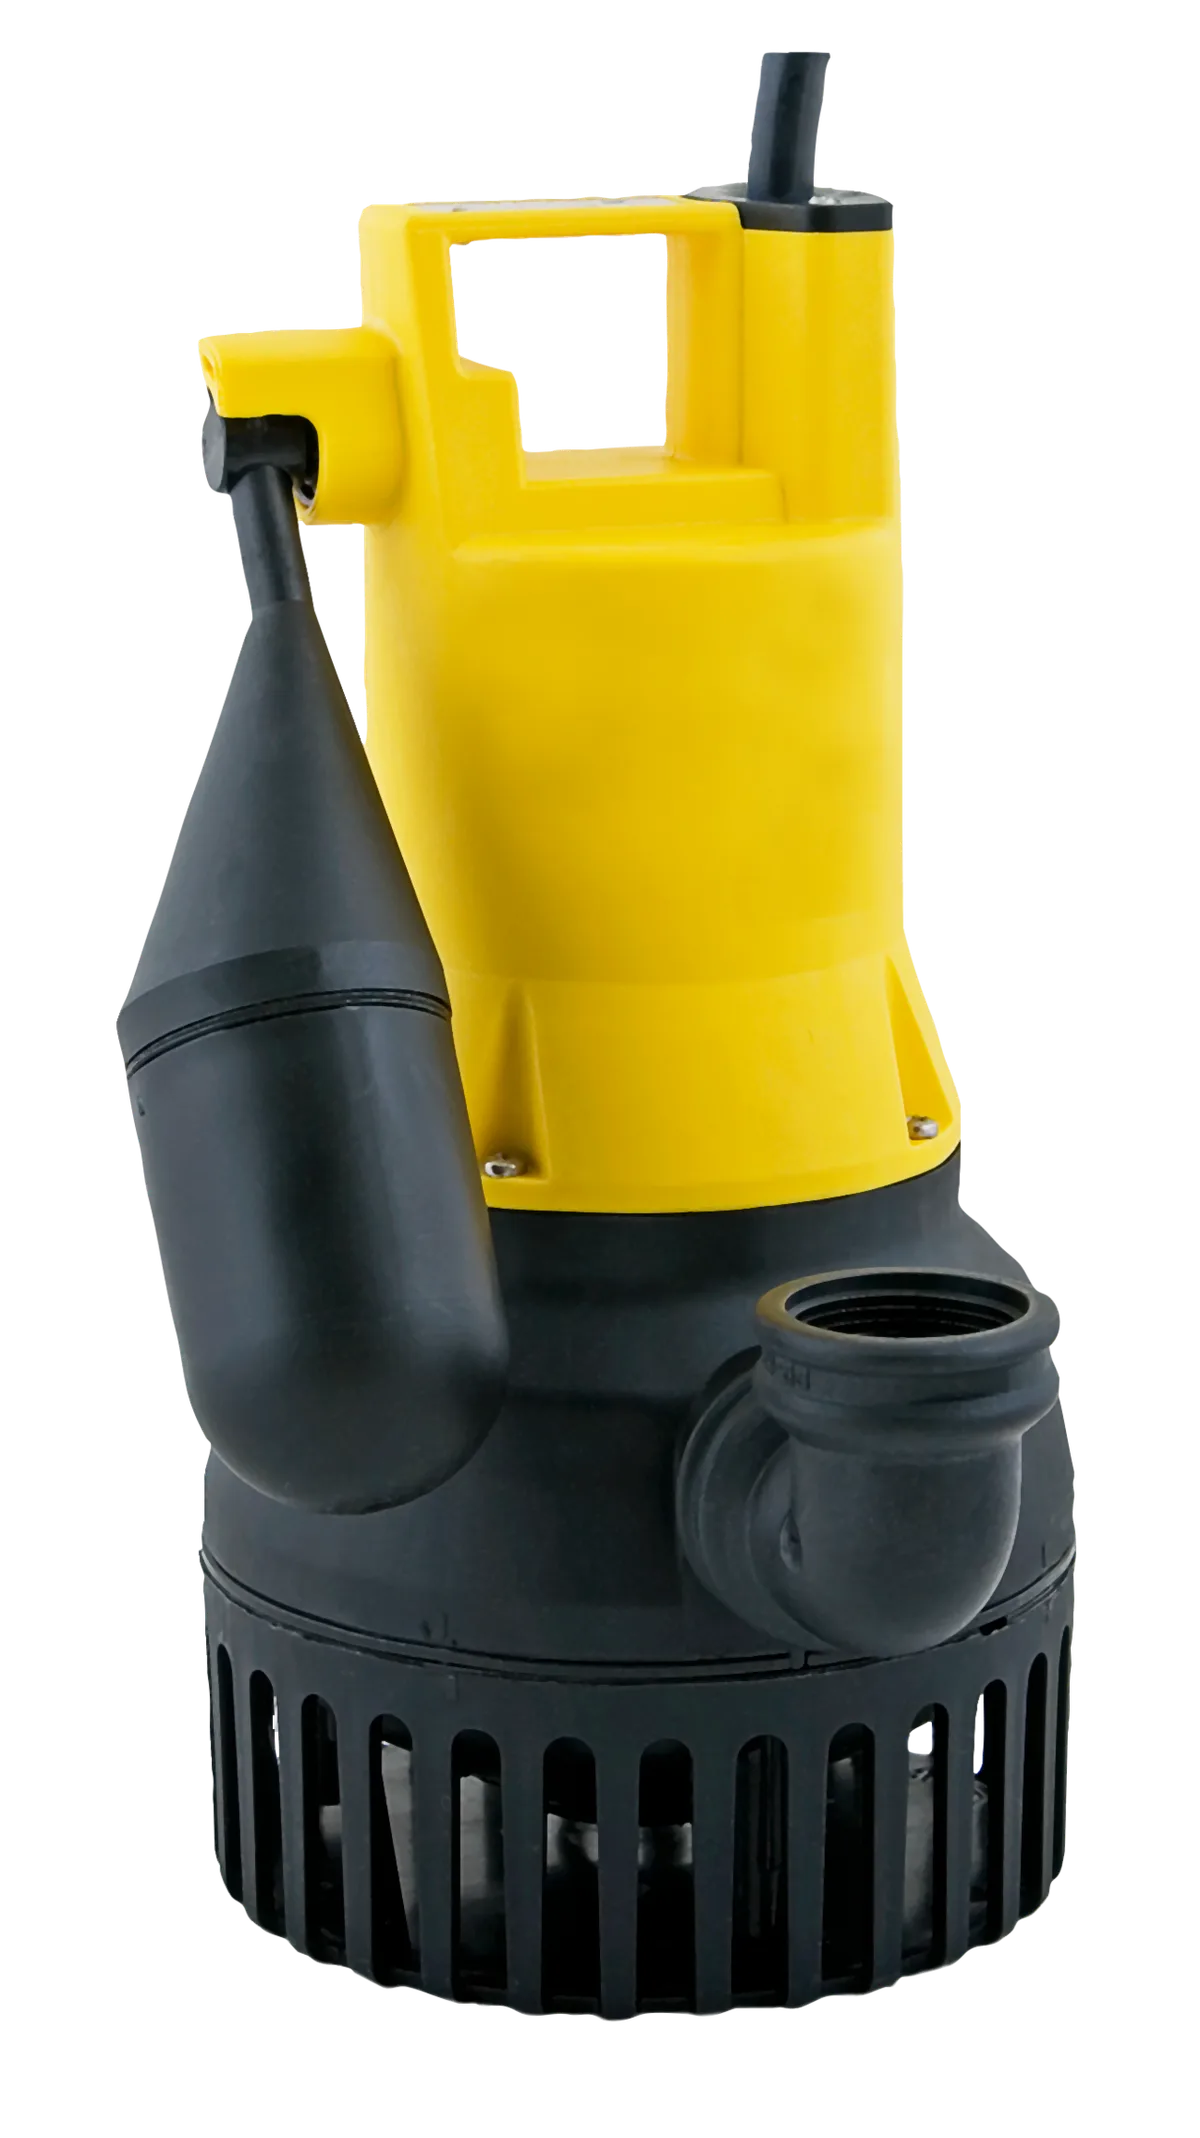
Image source: Wikimedia Commons / PumpExpert (CC BY-SA)
Dry running generates excessive heat that destroys mechanical seals and burns out motors rapidly. Conversely, an oversized hole creates massive water recirculation back into the basin. Your pump then cycles continuously without achieving proper shutoff head pressure or clearing the pit.
Warranty Implications of Unauthorized Modifications
Most manufacturers explicitly prohibit field drilling on pre-engineered thermoplastic housings as of 2026. Unauthorized modifications instantly void UL listings and product warranties regardless of installation quality. Factory-drilled relief ports are positioned precisely relative to internal volute geometry for optimal performance.
Drilling through cast iron housings requires specialized cobalt bits and introduces metal shavings into the impeller chamber. These debris particles cause immediate cavitation damage or seal failure upon first startup. Professional waterproofing contractors typically replace non-compliant units rather than risk liability from modified equipment.
Understanding these mechanical risks helps explain why diagnostic codes appear when appliances operate outside designed parameters. Proper sizing ensures reliable activation during critical low-water events without compromising system integrity.
How to Safely Drill or Verify Your Sump Pump Bleed Hole
Safe modification begins with locating the official installation manual for your exact pump model. Manufacturer documentation specifies whether field drilling is permitted and provides precise coordinates. If no weep hole exists and specs allow one, gather appropriate tools before proceeding.
| Tool | Purpose | Specification |
|---|---|---|
| Cobalt drill bit | Cast iron penetration | 3/16 inch or #7 |
| Titanium bit | Thermoplastic housing | 3/16 inch standard |
| Center punch | Prevents bit wandering | Steel tip |
| Deburring tool | Removes sharp edges | Internal and external |
Mark the location exactly one to three inches above the check valve fitting. This placement ensures air escapes while preventing sediment accumulation at the lowest point. Use a center punch to create a starter dimple and prevent dangerous bit walking on curved surfaces.
Drilling Technique and Post-Installation Verification
Drill at a 45-degree downward angle toward the basin floor to direct spray away from electrical components. Apply steady moderate pressure without forcing the bit through the casing wall. Stop immediately upon breakthrough to avoid damaging internal impeller clearances or motor windings.
Deburr both interior and exterior edges thoroughly to eliminate turbulence points and injury hazards. Test cycle the pump multiple times to verify a consistent pencil-sized stream exits the hole. Weak bleeding indicates partial blockage requiring careful reaming or complete unit replacement.
This verification process mirrors how technicians approach troubleshooting appliance faults systematically. Skipping validation steps often leads to callback failures during heavy rain events when reliability matters most.
Common Weep Hole Questions Answered
Can I use existing factory holes instead of drilling new ones?
Factory-drilled weep holes are always preferable to field modifications when present. Manufacturers engineer these ports at optimal locations relative to internal hydraulics and structural weak points. Inspect the pump housing carefully near the discharge port before attempting any drilling work yourself.
What happens if my weep hole becomes clogged over time?
Mineral deposits and iron ochre frequently obstruct small relief ports in hard water regions. Annual maintenance inspections should include verifying unobstructed flow using a thin wire probe. Blocked holes restore air lock conditions identical to having no relief port installed initially.
Does pedestal pump design require different weep hole sizing?
Pedestal pumps rarely need weep holes because their intake sits below the water line permanently. Submersible units face air trapping risks due to horizontal discharge orientations and check valve placement. Consult your specific pedestal model manual rather than applying submersible standards universally across all pump types.
Is there a maximum safe distance above the check valve?
Positioning the hole more than six inches above the check valve defeats its anti-airlock purpose entirely. Trapped air columns form between the valve and an overly high relief port during off cycles. Keep the opening within one to three inches vertically for reliable priming assurance every cycle.